
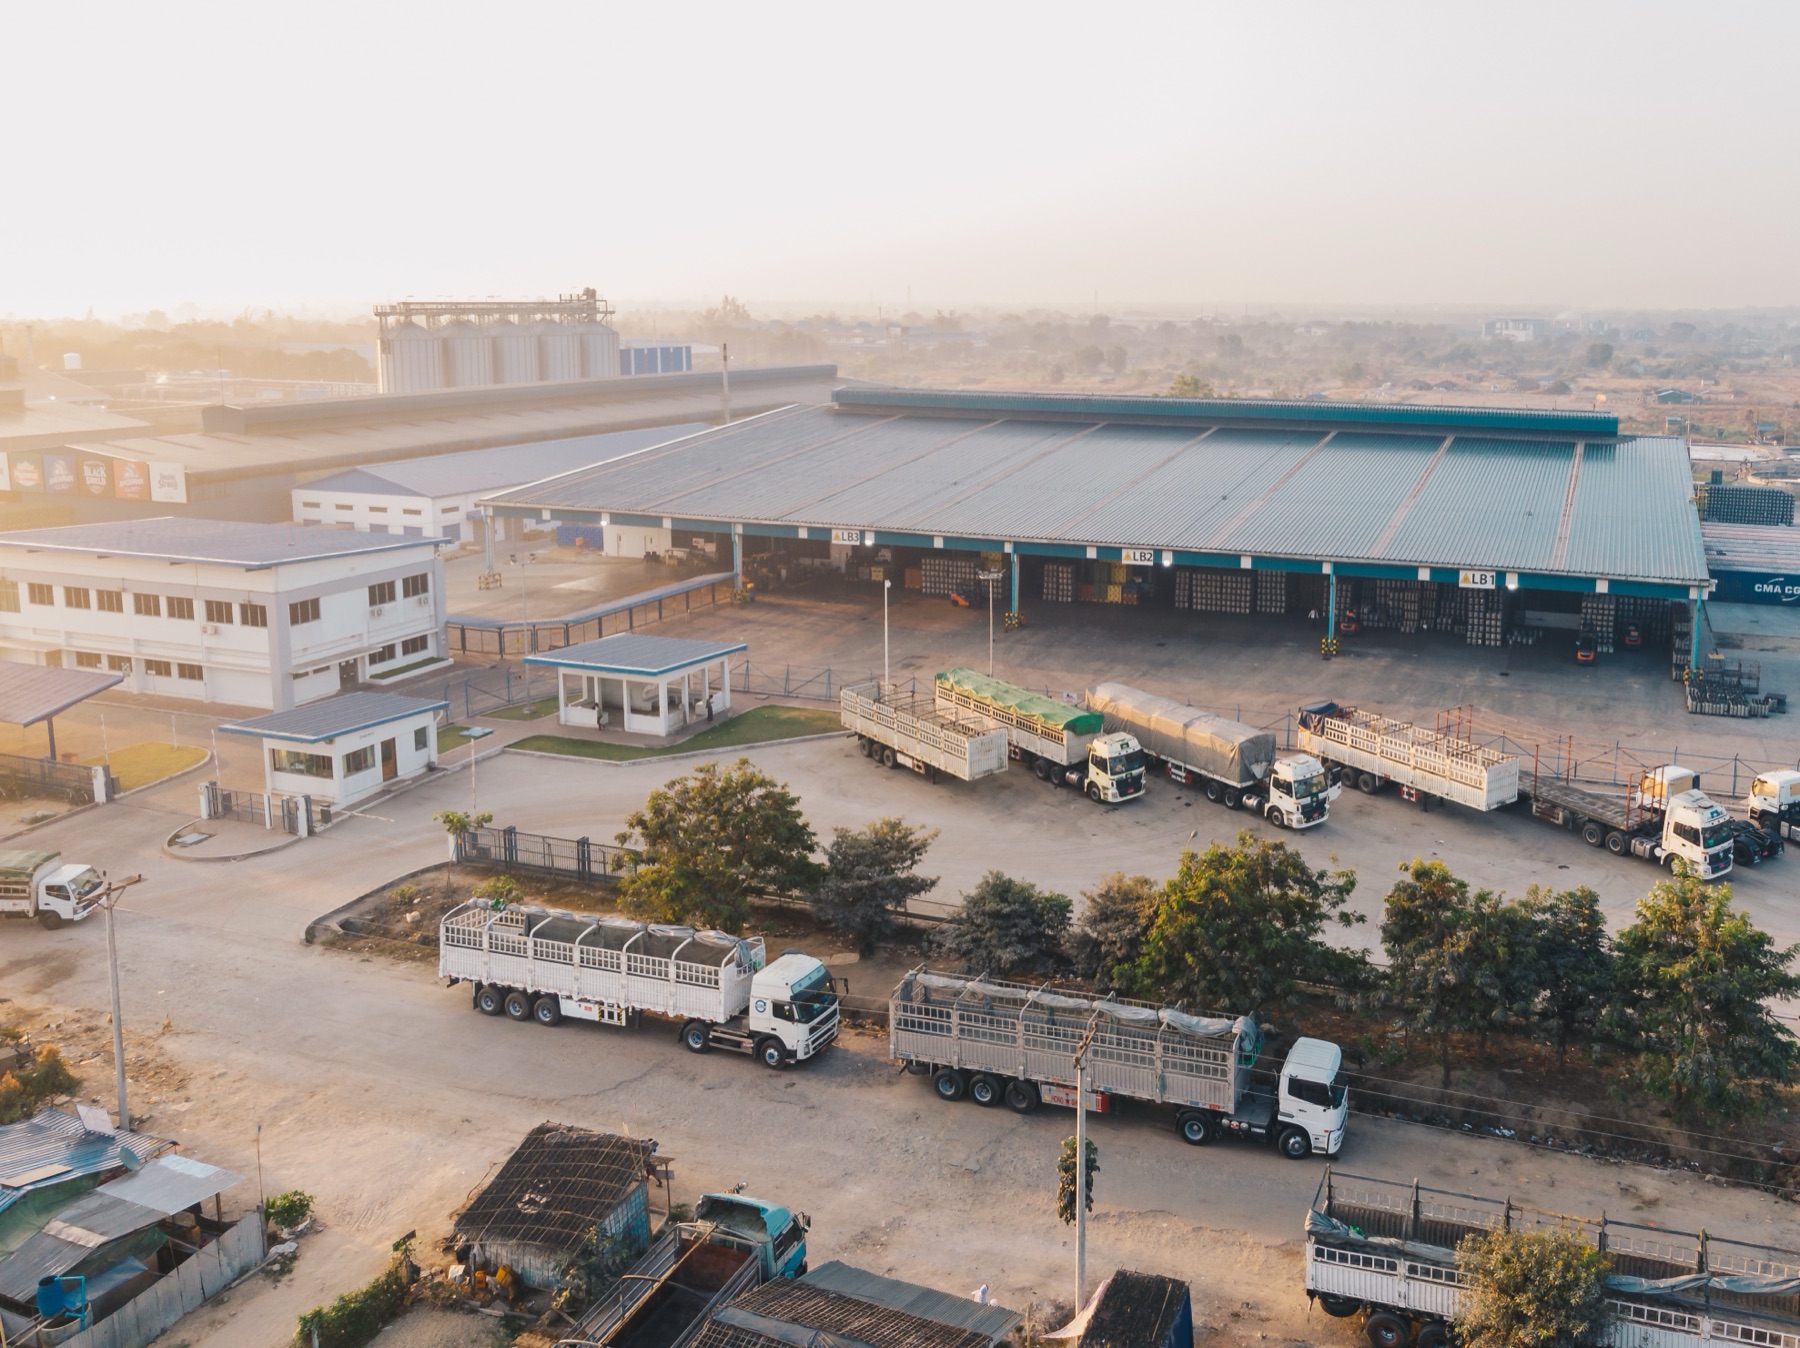
Industrial Zones and Manufacturing Plants
At a factory, one late shuttle means a shift of lost output on the line. vitaRoute builds the shuttle operation of multi-shift, out-of-town plants backwards from the shift start time.
The industry's problem
Why is shuttle service hard in this sector?
Organized industrial zones sit outside the city centre; public transport is either absent or out of step with shift times. For employees, the shuttle is in practice the only way to get to work. That means running an operation of hundreds of people and dozens of vehicles every day with zero tolerance.
What makes it hard is that the plan is never built once and finished. The same fleet carries several different passenger groups in a day; at every shift change the roster, the routes and the vehicle assignments have to be rebuilt. Leave, sick leave, transfers and new hires shift the list every week.
Managed by hand, the cost shows up in three places: the fixed cost of vehicles running half full, fuel on long routes, and a production line that waits at every disruption.
- Passenger groups that change up to three times a day
- Out-of-town location: long routes, a high share of fuel cost
- A large number of vehicles, each with its own fixed cost
- Zero tolerance at shift start
In the field
A day at a three-shift factory
- 05:15
The morning shift is collected
The morning shift's vehicles set out in the early hours on routes calculated with that hour's traffic data. The arrival time is worked out backwards from the shift start at the gate.
- 13:45
Shift change: same fleet, new passengers
The vehicles that dropped off the morning shift collect the afternoon shift. The same fleet serving two separate passenger groups is built into a single plan; the vehicle count is set according to the shift roster.
- 21:30
Night shift and return trips
For the night shift, both inbound and outbound trips are planned. The outbound routes are re-sequenced according to the order in which employees head home.
- Month-end
Timesheet and cost close
The timesheet comes out of completed trips on its own. You can see how much fuel and how many km each line used, route by route.
No tolerance at shift start. The plan is built with that in mind.
What does vitaRoute do in this sector?
Industrial Zones and Manufacturing Plants
Planning backwards from the shift time
Each shift is built as a plan of its own. The arrival time is fixed to the shift start at the gate, and travel times are taken from that hour's traffic data. 07:30 in the morning and 23:00 at night are not planned with the same duration.
- A separate plan for each shift
- Travel times from the traffic data of that shift's hour
- Arrival time worked backwards from the shift start
A new plan the same day when the roster changes
The shift roster is bulk-uploaded with Excel or pulled from your existing system; the plan is rebuilt within minutes. Occupancy per vehicle is tracked live, and a line that keeps running half empty shows up as a vehicle that can be taken out of the plan.
- Shift roster bulk-uploaded with Excel
- Live occupancy per vehicle
- Vehicles that can be removed from the plan are clearly visible
Fuel and kilometre control
On long routes, fuel is the deciding cost item. Consumption is tracked per line; how much a fuel price hike will affect each route is calculated before the hike arrives.
- Fuel consumption per route
- Effect of a price hike per line
- Km and cost in a single report
Before / after
Four situations in the field, two approaches
The shift roster changed at the last minute
Managed by hand
Rebuilding the plan takes a day; the old plan runs that day and some employees get home late.
With vitaRoute
The roster is uploaded, the plan is rebuilt within minutes and reaches the vehicles the same day.
A line keeps running half full
Managed by hand
Nobody notices; the vehicle runs every day at its fixed cost.
With vitaRoute
Occupancy is tracked per vehicle. A half-empty line is flagged as a line that can be merged.
The fuel price went up
Managed by hand
The impact is noticed on the invoice at month-end.
With vitaRoute
The effect of the hike on each line is calculated in advance; you know which route will be hit hardest.
A vehicle was late this morning
Managed by hand
The plant phones the driver, and the line waits until the cause is found.
With vitaRoute
Planned and actual are compared; a line with chronic delays is corrected in the next plan.
The most used solutions in this sector
Industrial Zones and Manufacturing Plants
Explore
Other sectors
Frequently asked questions
Each shift is a planning problem in its own right. vitaRoute builds a separate plan for every shift and shares the same fleet across shifts; the vehicle count is set not by the busiest shift but by the real need of each shift.
Let's build the first plan together with your factory's shift roster.
Upload your employee list and shift times, and see your first plan in minutes.